Core Manufacturing Processes & Quality Control of Stainless Steel Shaped Wire for Petrochemical and Seawater Desalination
Release time:
2026-09-26
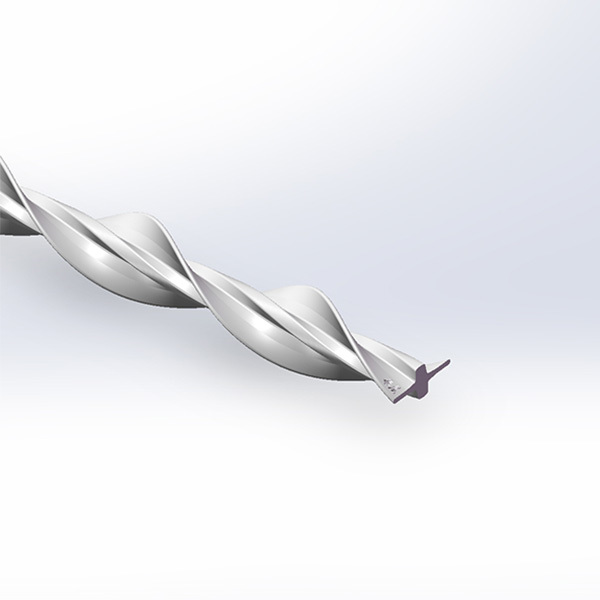
Stainless steel wedge V-wire, triangular wire and trapezoidal shaped wire for petrochemical and seawater desalination filter components are mainly manufactured by cold plastic forming at ambient temperature. The two dominant forming technologies are roll drawing (Turks Head multi-roll profiling) and carbide die drawing. The full workflow includes billet pretreatment, intermediate heat treatment, surface finishing and online inspection to tightly control cross-section tolerance, residual stress and surface cleanliness, securing corrosion resistance under high chloride and sulfur-containing service conditions.
Roll Drawing (Combined Multi-roll Rolling & Drawing, Industry Primary Choice)
Qualified stainless steel wire rod is fed into progressive grooved roll sets for continuous rolling and traction to gradually form wedge or triangular profiles. Roll dies adopt rolling friction with low wear and large single-pass reduction, cutting intermediate annealing cycles. Equipped with laser online dimension monitoring and closed-loop adjustment, it delivers stable dimensional tolerance and minimal edge burrs. It is widely applied for mass production of wedge wire for Johnson screens and oil sand control screens. 2205/2507 duplex and 904L high-alloy shaped wire mostly adopt this process to balance forming precision and corrosion resistance retention.
Carbide Die Drawing
Billet is pulled through custom carbide shaped dies pass by pass. It delivers superior dimensional accuracy and regular profile contour, suitable for small-batch precision flat wire with complex cross-sections. The drawback lies in sliding friction between wire and die, which accelerates work hardening and leaves high residual stress. Stress-relief heat treatment is mandatory after forming. It is adopted for custom small-size shaped wire for precision petrochemical filter elements instead of large-tonnage wedge wire mass production.
Auxiliary Key Procedures
Billet pretreatment: Wire rod is pickled and alkaline cleaned to remove scale and grease; high-alloy grades require strict control of sulfur and phosphorus impurities to avoid forming cracks.
Intermediate bright heat treatment: 316L austenitic steel adopts hydrogen-protected bright annealing. 2205/2507 duplex steel requires solution treatment followed by water quenching. Prolonged holding within 600–1000℃ must be avoided to prevent brittle sigma phase, which severely impairs pitting resistance. Segmented annealing is required between multi-pass forming to release accumulated cold-work stress, otherwise stress corrosion cracking risk rises sharply.
Surface finishing: Electropolishing is preferred for desalination and chemical service to eliminate micro scratches and iron contamination and reduce chloride pitting initiation; mechanical polishing is acceptable for general service.
Inspection: Inline dimensional monitoring plus metallographic test, pitting corrosion test and tensile test for finished goods. Material certificates are issued to meet overseas CE and ASTM project requirements.
Process Selection & Foreign Trade Notes
Roll drawing is the preferred option for standard 316L wedge wire with competitive cost and fast delivery. Die drawing is selected for high-alloy, high-precision small-batch custom orders. For export contracts, overseas project owners impose stricter review on residual stress, surface purity and metallurgical reports. Innovate Wirerod (Taizhou) New Materials supports both roll drawing and die drawing lines, supplying custom V-type, triangular and trapezoidal shaped wire for Middle East desalination and South America oil sand control projects. Stable manufacturing process and complete inspection documentation become core strengths for domestic manufacturers to raise product premium and penetrate high-end global engineering markets.
More news


Contact Us
E-mail:
Wechat:+8613365215016
WhatsApp: +8613365215016
Address:B3-01, Zhangguo Town Science and Technology Park, Xinghua City, Taizhou City, Jiangsu Province
Copyright:Innovate Wirerod (Taizhou) New Materials Co., Ltd.

Message